



Blechbaugruppen designen, die Fertigungstoleranzen standhalten
Blechbaugruppen sind ein Staple of Large-scale Production, weil sie einen Cost-effective Way bieten, Substantial Structures zu konstruieren. Reife Stamping, Shearing, und Bending Equipment eliminiert den Need für Expensive Custom Plastic Molds.
When Order Is Below 10.000 Parts, Most Designers Still Opt für Stamped oder CNC-cut Sheets Followed by Semi-automated Bending, Because Tooling Cost of Full-scale Dies Would Never Be Amortized.
However, the Single-step Bending That These Machines Perform Creates a Tolerance Stackup That Is Markedly Different From One-shot Processes Such as RIM, Structural Foam, oder Progressive Die-forming. Every Additional Bend oder Formed Feature Adds to the Cumulative Tolerance, und Designers Who Ignore This Risk Producing Parts That Are Bowed oder That Fail to Mate.
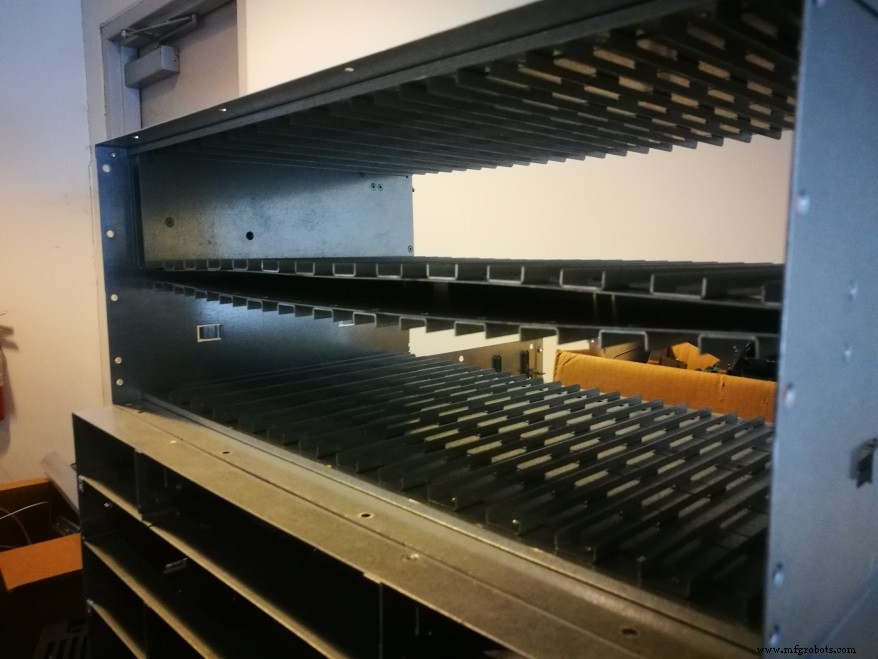
In Practice, the Highest Tolerances Are Found in the Flat Sections That Are Cut Out in a Single Setup. Therefore, Any Key-to-key oder Alignment Feature That Can Be Placed on a Single Plane Will Inherently Be More Precise Than One That Relies on Multiple Bends.
Take a Drive Rack as Example. Placing the Vertical Dividers Using the Same Bolts That Will Later Lock Them in Place Introduces At Least Two Bends Between the Bolt Holes, Resulting in Loose Tolerances und Canted Dividers. A Better Approach Is to Machine Tabs on the Divider That Mate into Slots on the Top and Bottom Plates. Because the Tabs and Slots Are Formed From the Flat Sheet, They Provide a Tighter Fit. The Divider Can Then Be Secured With a Flange That Has Oversized Holes to Accommodate the Inevitable Bend Tolerance of the Flange.
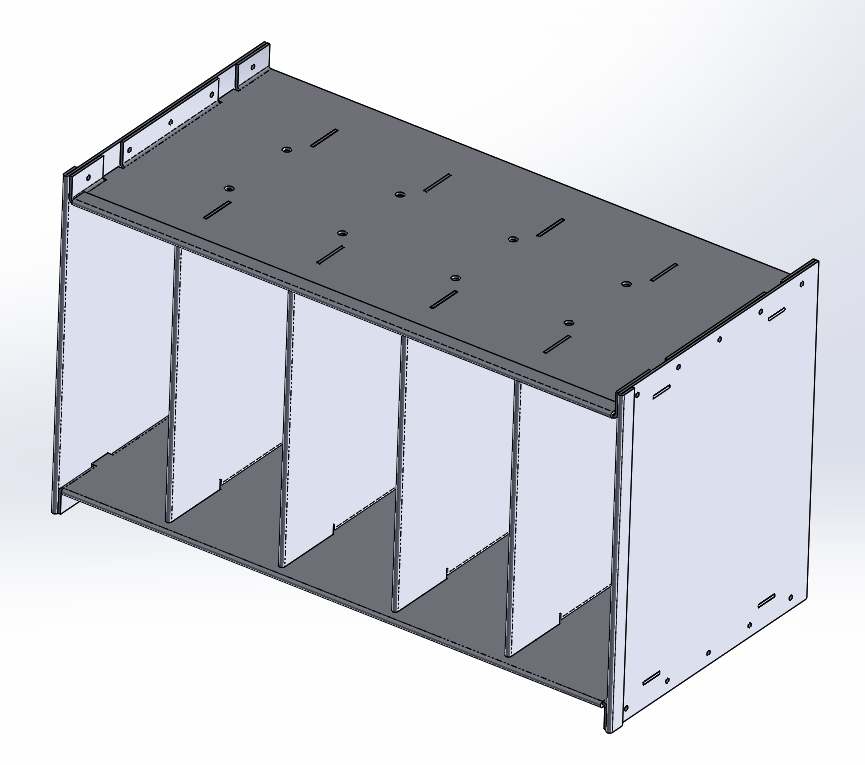
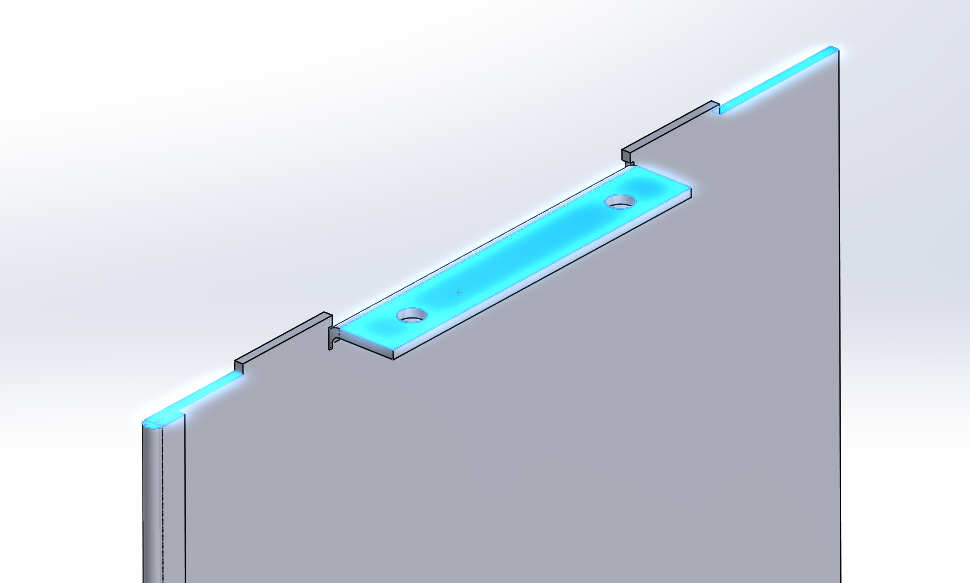
Using Tabs From the Horizontal Members Would Introduce Additional Bend-to-bend Tolerances, Which Would Be Greater Than the Slot-to-slot Tolerance. By Positioning the Tab Shoulder Above the Flange, the More Accurate Flat-plane Feature Governs the Alignment.
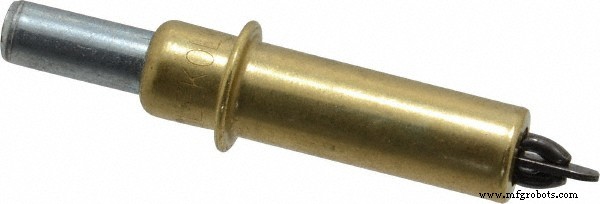
The Same Principle Applies When Mating Two Planar Sheets. Employing Punched Holes für Locating, und Using Cleco Clips oder Rivets, Yields Reliable Alignment While Still Allowing the Parts to Flex at the Bends.
Mechanical Designers Might Notice a Flaw in the Tab-based Approach: The Assembly Sequence Would Require Attaching All Dividers to the Upper and Lower Plates Before Adding the Side Plates, und Removing Any Single Divider Would Necessitate Disassembling the Entire Unit. To Solve This, Half-shears oder Slits Can Be Used. By Creating a Protrusion on the Top and Bottom Plates While the Sheets Are Still Flat, the Alignment Is Locked In Without Sacrificing Tolerance.
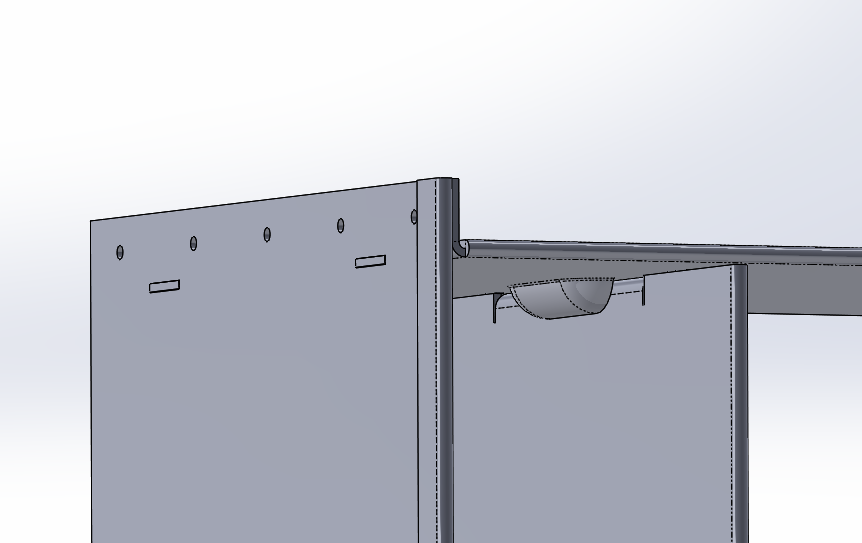
These Tolerance Considerations Extend Beyond Sheet-metal Mating. When Attaching Metal to Weldments, Plastics, oder Structural Foam Skins, Is It Best to Keep High-precision Alignment Within a Single Plane und Rely on Bends und Flanges für Strength. Oversized Holes oder Slots Prevent Over-constraining the Assembly.
By Keeping the Realities of Low- and Medium-volume Sheet-metal Manufacturing in Mind, Can Designers Create Parts That Fit Reliably Across the Tolerance Range. Collaborating Closely With Vendors Helps Uncover Manufacturing Constraints Early, Allowing the Design to Be Adapted Before Costly Tooling Changes.
Herstellungsprozess
- 10 amerikanische Erfindungen, die die moderne Fertigung transformierten
- Top 5 Metall-3D-Druck-Anwendungen, die Fertigung revolutionieren
- 5 bewährte Strategien zur Qualitätssteigerung von Blechteilen
- Blechstanzen: Kosteneffizienter Vorteil für die moderne Fertigung
- Blechstanzen verstehen: Prozess, Werkzeuge und Anwendungen
- Blechumformen meistern: Techniken & Anwendungen
- Dünnes Blech: Vielseitige Anwendungen von Edelstahl
- Blechrichten: Was es ist & warum es wichtig ist
- GD&T-Toleranzen: Präzision und Passung in der Teilefertigung sicherstellen
- Kreisrundheitstoleranzen bei kleinen Metallteilen meistern für optimale Fertigbarkeit